

Great Taste Starts with Great Quality
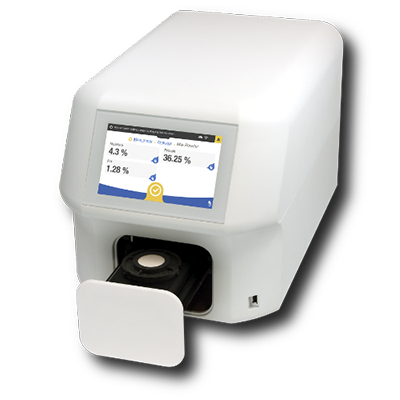
The SpectraAlyzer FOOD is a state-of-the-art NIR food analyzer designed for fast, accurate, and reagent-free food quality control. Ideal for food production and processing, it measures critical quality parameters—moisture, protein, fat, sugar, starch, acidity, salt, and ash — in under 45 seconds, helping manufacturers ensure consistent product quality and efficient production.
By delivering precise near-infrared (NIR) analysis at or near the production line, the SpectraAlyzer FOOD enables food processors to reduce production costs, maintain high yields, and meet global quality standards. Its rugged design guarantees reliable operation even in environments with temperature fluctuations, vibrations, or dust.
Key Features and Benefits
-
Rapid NIR Food Analysis: Obtain quantitative results for major food quality parameters in under 45 seconds.
-
Reagent-Free Operation: No sample preparation or chemicals required, reducing operational costs.
-
Versatile Sample Handling: Supports powders, pastes, slurries, and liquids using closed, open, viscous, slide, or disposable cups.
-
User-Friendly Interface: Intuitive touchscreen operation with hygienic glass touch surface for easy, safe handling.
-
Compact & Flexible Design: Perfect for bench-top or at-line applications.
-
Pre-Loaded Calibration Models: Quick setup and immediate operation with numerous mathematical models for diverse food products.
-
Webserver & Cloud Connectivity: Access and monitor instruments remotely via LAN or internet for automated logging, reporting, and database storage.
-
Reliable NIR Technology: High sensitivity and long-term stability using SpectraAlyzer sample–reference optics.
Applications
-
Food Production: Dairy, bakery, confectionery, sauces, and beverages.
-
Ingredient Testing: Flours, oils, sugar, starches, and powders.
-
Quality Control: Moisture, protein, fat, sugar, acidity, salt, and ash analysis in processed and raw foods.
With the SpectraAlyzer FOOD, manufacturers achieve precise, reproducible, and cost-effective food quality control, ensuring every product meets the highest standards and satisfies consumer expectations.